Shipment · 22 Oct 2026
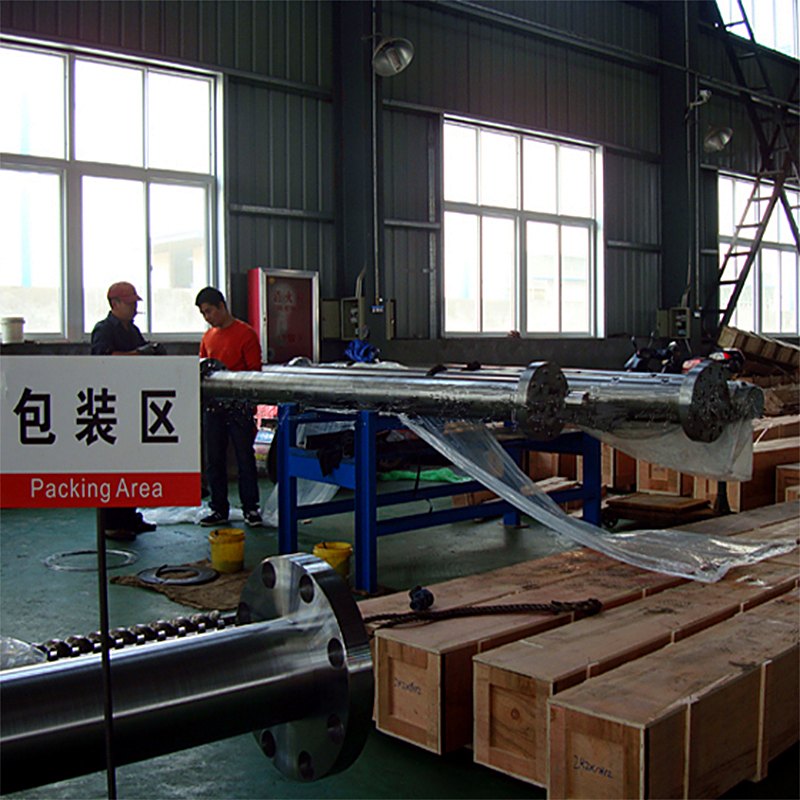
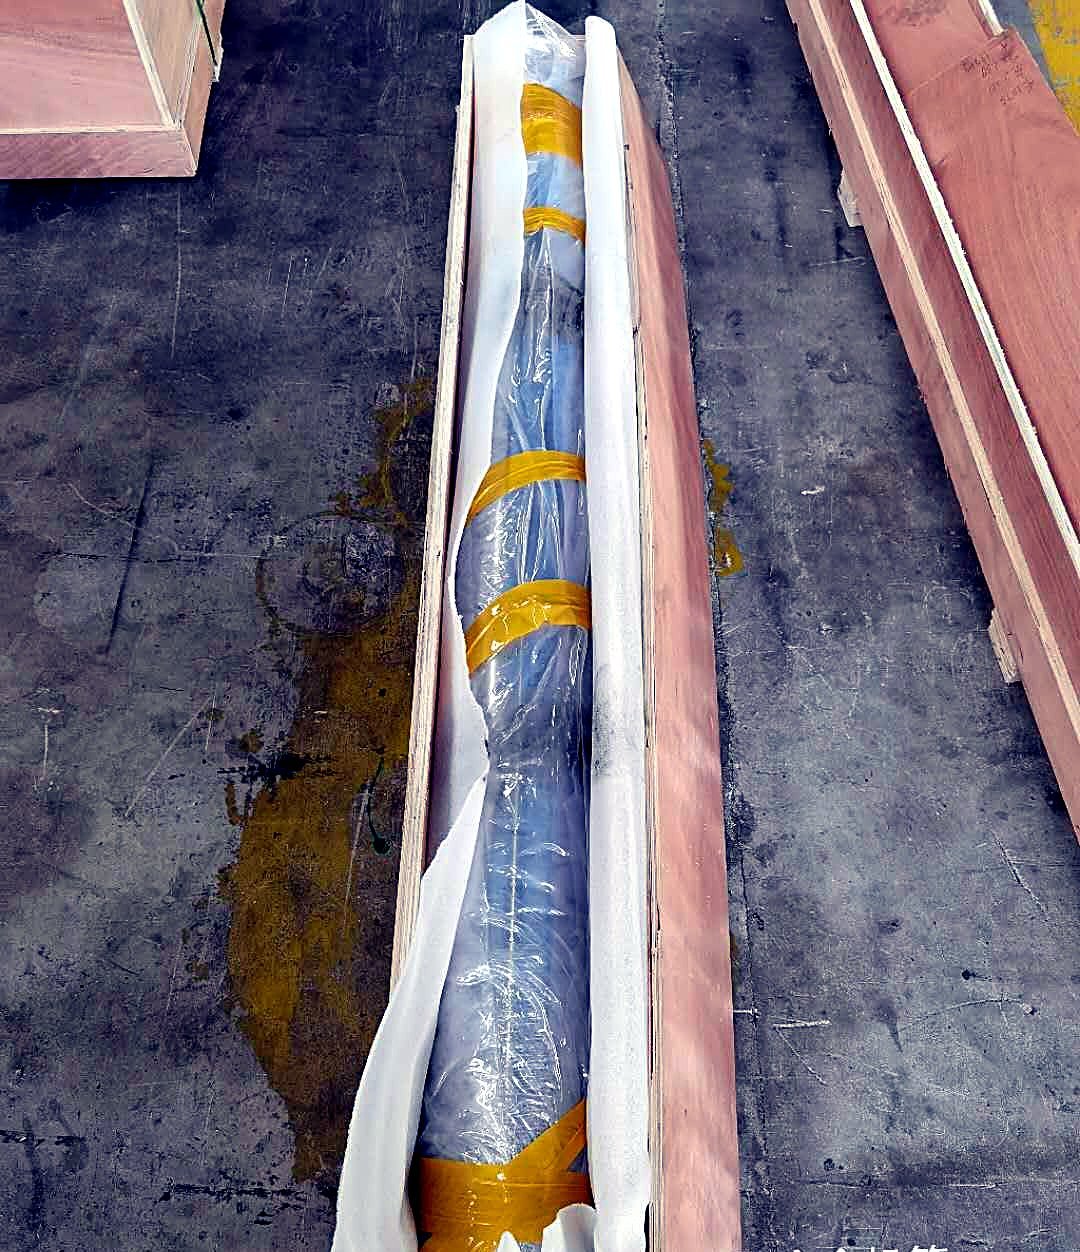
From rough turning to flight polishing - a look at the current twin screw batch on our workshop floor.
Steel bar to finished twin screw passes through five gates in our workshop. Here is what happens at each one, and why the order matters.
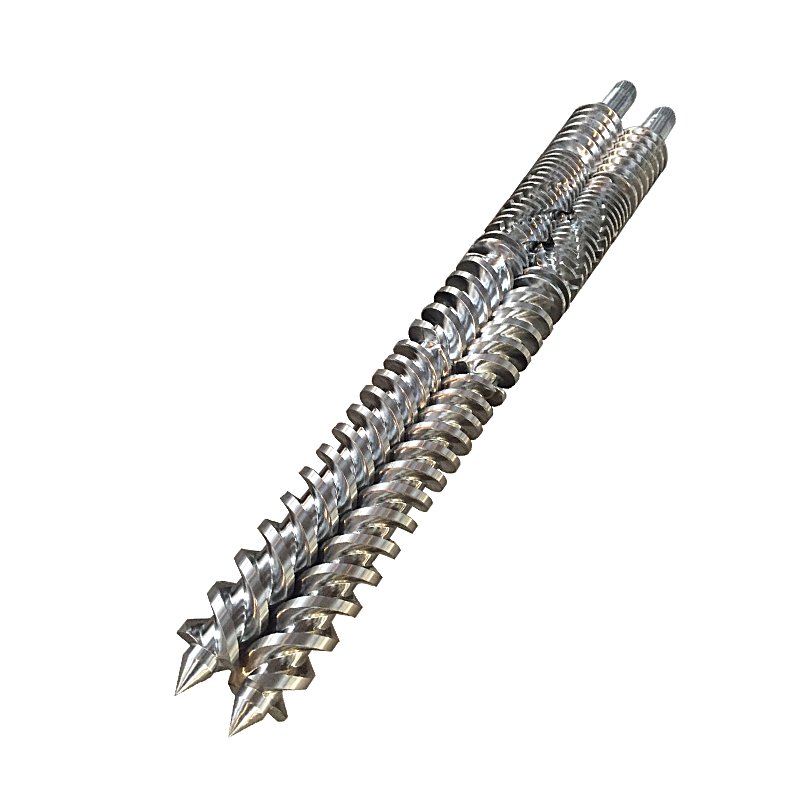
The billet is rough turned close to final geometry, then stress relieved. Skipping this step is the commonest reason a screw that measured perfectly in the machine arrives bent after heat treatment - internal stress released later has nowhere to go.
CNC thread milling holds the pitch and flight width consistently along the whole length. This is where the compression profile - feed, compression, metering - is cut, and it is the part most sensitive to your resin.
We nitride in-house, in four gas nitriding furnaces, together with four centrifugal bimetallic casting furnaces for alloy-lined bores. Keeping heat treatment inside our own building is why we can quote realistic lead times instead of promising dates that depend on a subcontractor's queue.
Flights are polished so material does not hang up and degrade, then the screw is measured again after heat treatment - because a part is only finished when it has been through its final process and still measures true.
Around 30–40 days after drawing approval for most twin sets, longer for large diameters or bimetallic bores. Tell us your machine and resin and we confirm a date together with the quotation - we would rather give you an honest week than a fast guess.
Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.