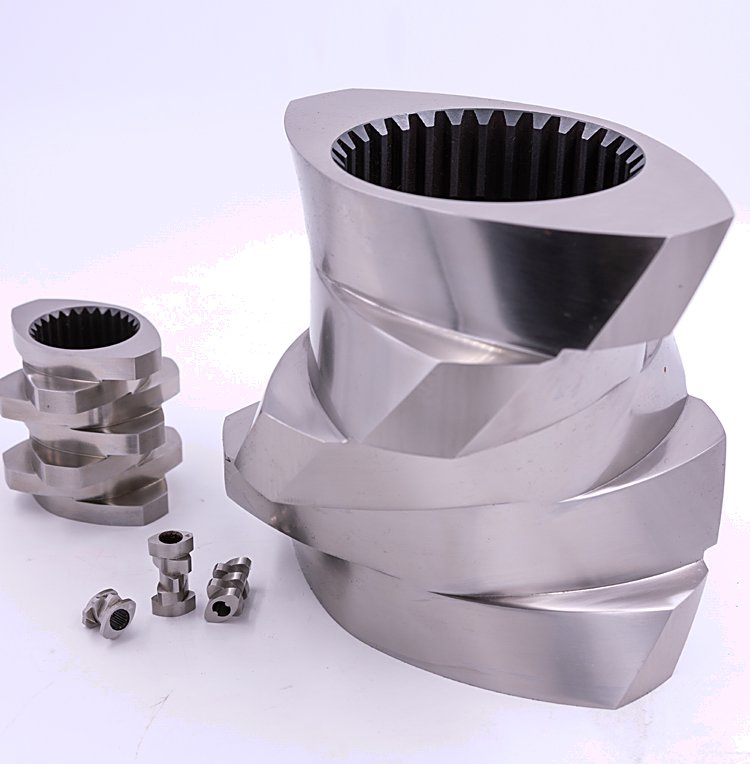
Modular segment barrels and sectional screw elements for twin screw extruders — replace only the worn section instead of the whole barrel, and keep spare segments on the shelf for fast changeovers.
A segment (sectional) screw barrel is a modular barrel built from short flanged sections instead of one long body. Twin screw extruders for compounding, masterbatch and recycling commonly use this design: each segment handles a different duty — feeding, conveying, kneading, venting or metering — and the most stressed sections wear first.
With a segment barrel you replace only the worn section, usually the kneading zone, instead of scrapping the entire barrel. That cuts replacement cost dramatically and lets you keep spare segments on site, turning a multi-week stoppage into a one-day changeover.
Intake section with optional grooved lining for positive feeding of powder and regrind.
Standard sections matched to your screw element layout and shaft spacing.
High-wear zones with bimetallic lining, where most of the abrasion happens.
Sections with vent ports for degassing, devolatilization and moisture removal.
End section machined for stable pressure build towards the die.
Conveying, kneading and mixing elements for modular screw shafts.
Complete barrel segment package for a new or rebuilt extruder.
Worn segments re-lined or replaced individually to restore geometry.
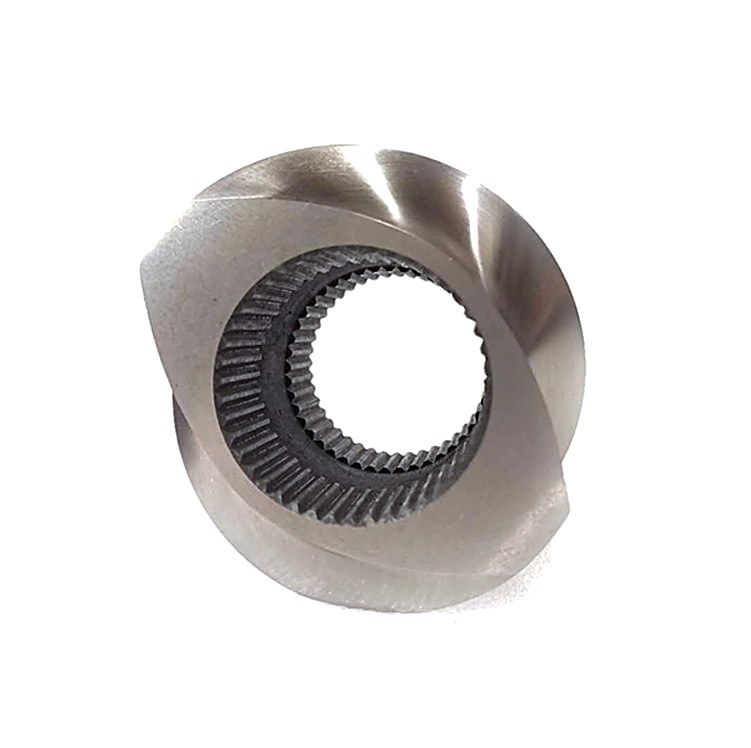
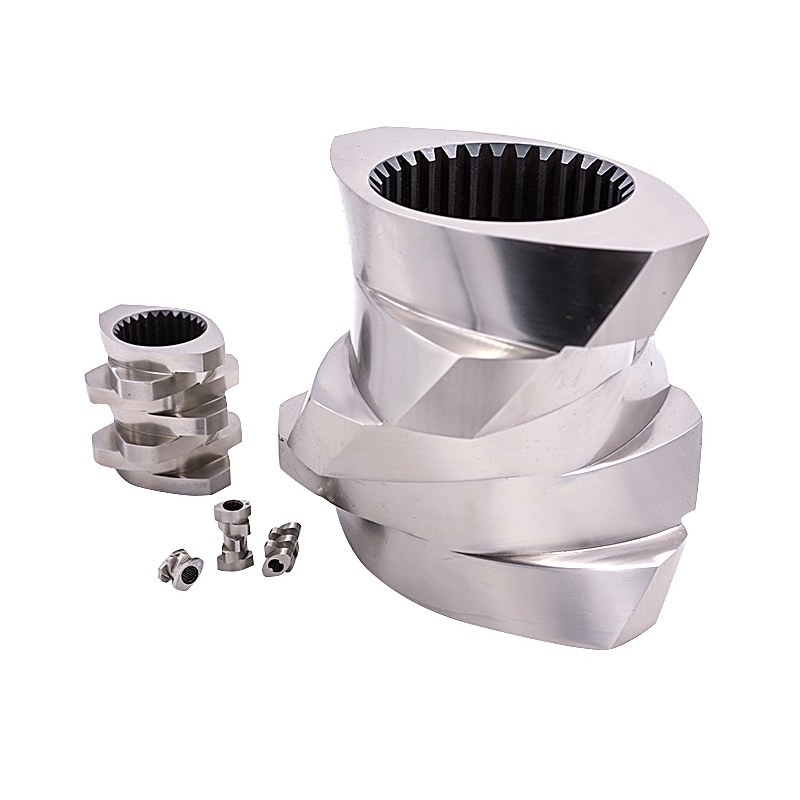
Conveying, kneading and mixing elements for co-rotating twin-screw compounders.
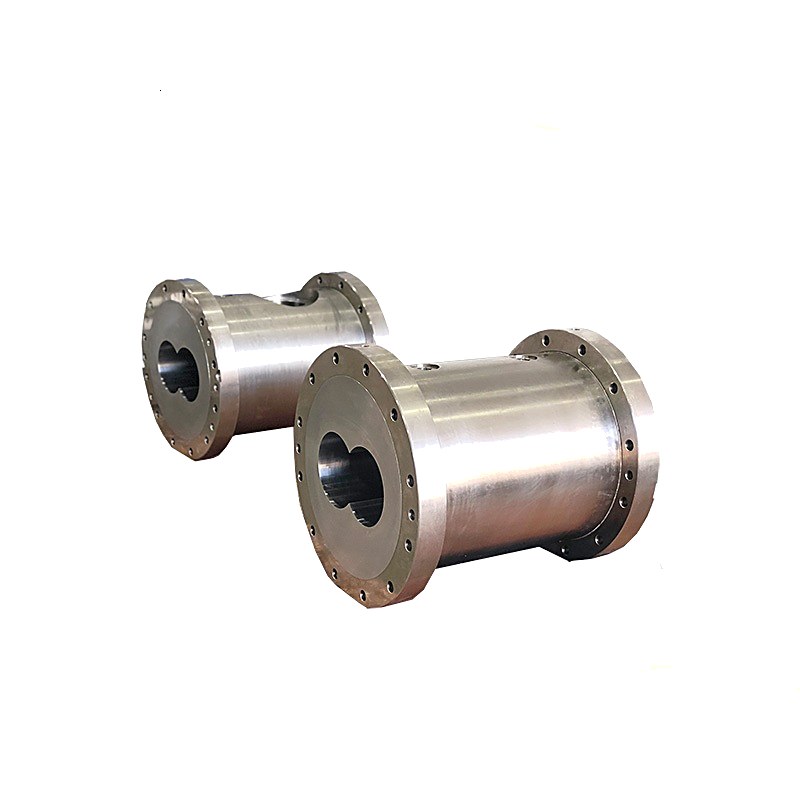
Modular barrel segments with bimetallic lining for compounding lines.
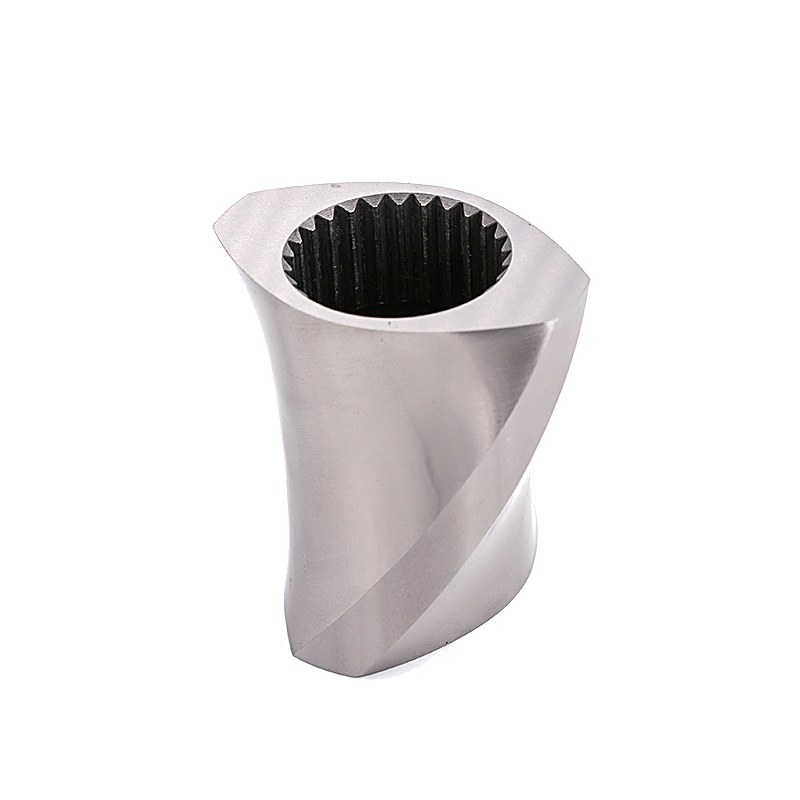
Shafts, spacers and fittings for segmented screw assemblies.
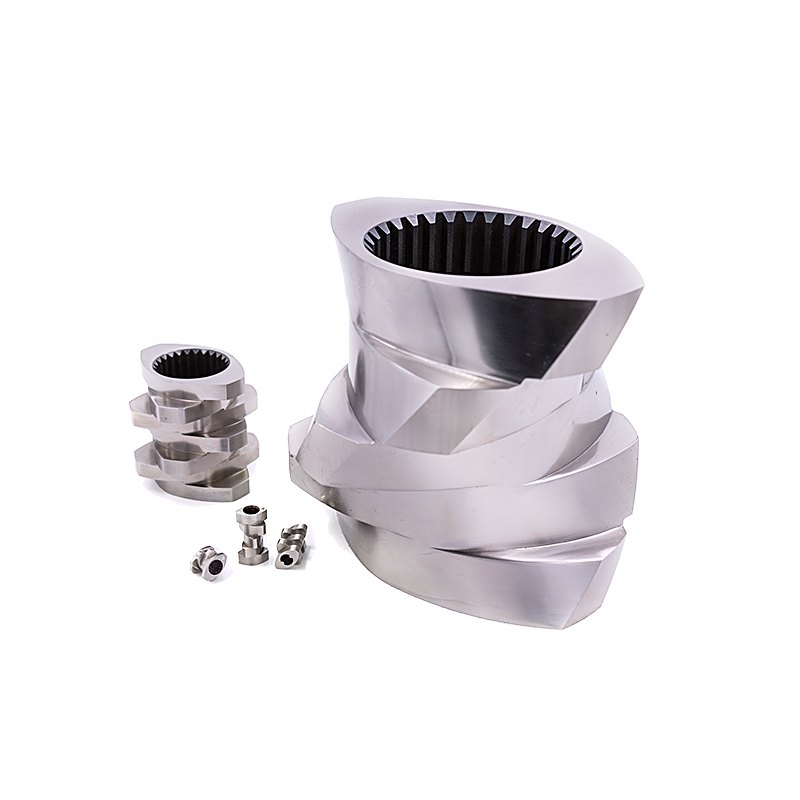
Replacement screw elements for co-rotating twin-screw compounding extruders, all major brands.
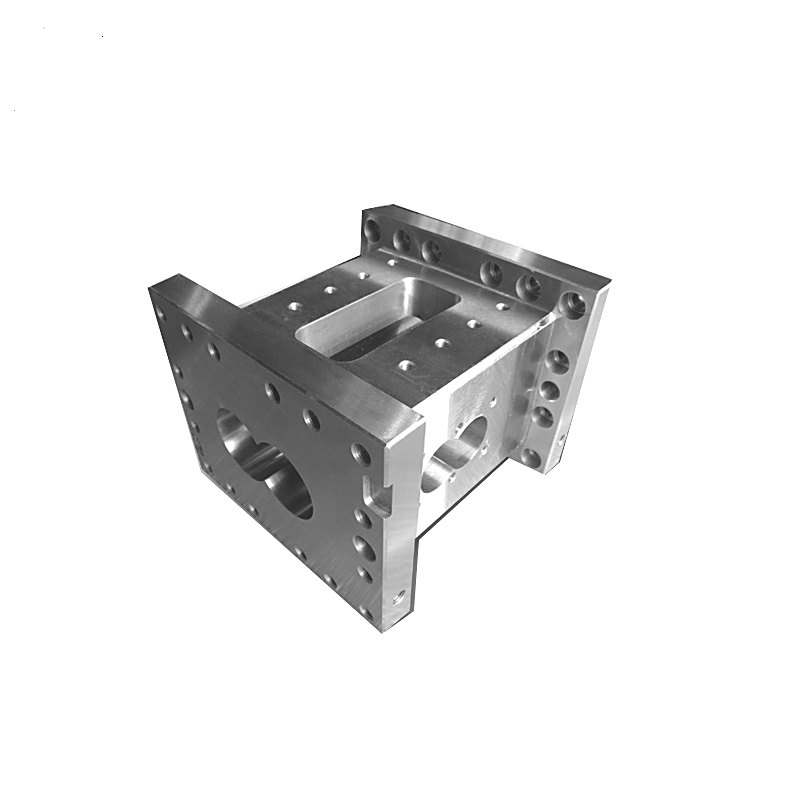
Modular twin-screw barrel segments with vent, side-feeder and closed configurations.
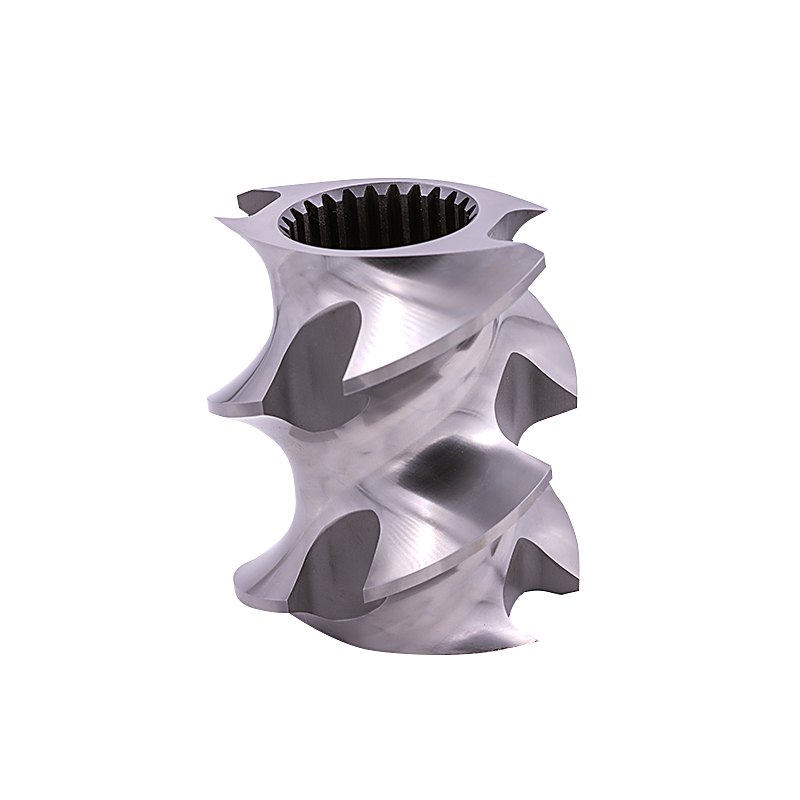
Hardened / bimetallic-coated kneading elements that survive 30–50% glass fibre duty.
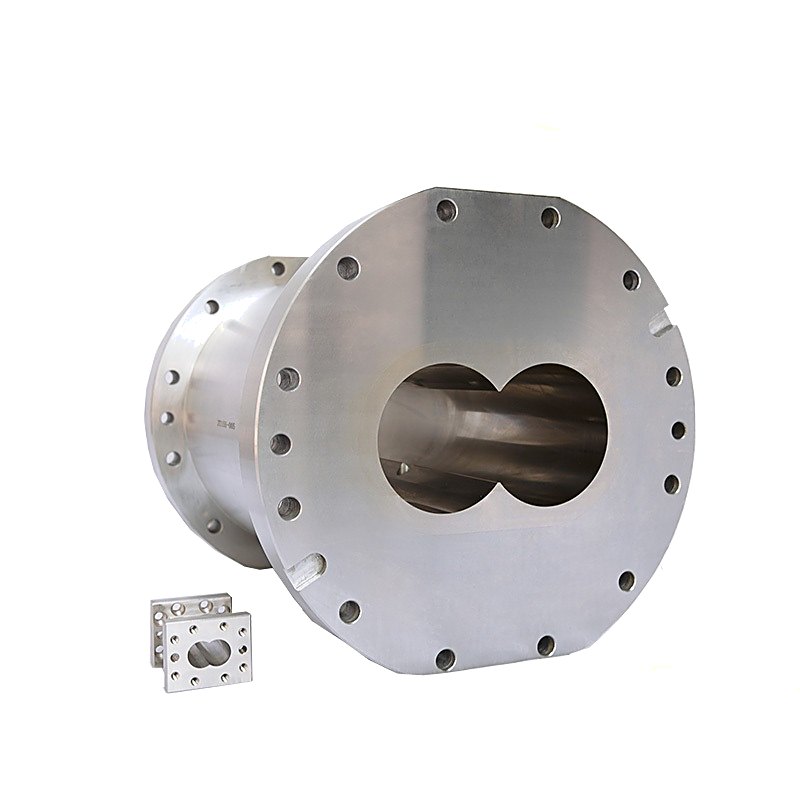
Barrel set configuration for masterbatch lines — side-feed to vacuum vent layout.
New models are added regularly — or send your drawing or worn sample for a custom build.
Standard ranges shown below. Non-standard sizes and custom geometry are built to your drawing or sample.
| Item | Specification |
|---|---|
| Application | Twin screw extruders — compounding, masterbatch, recycling |
| Segment Length | Standard modular lengths, custom lengths on request |
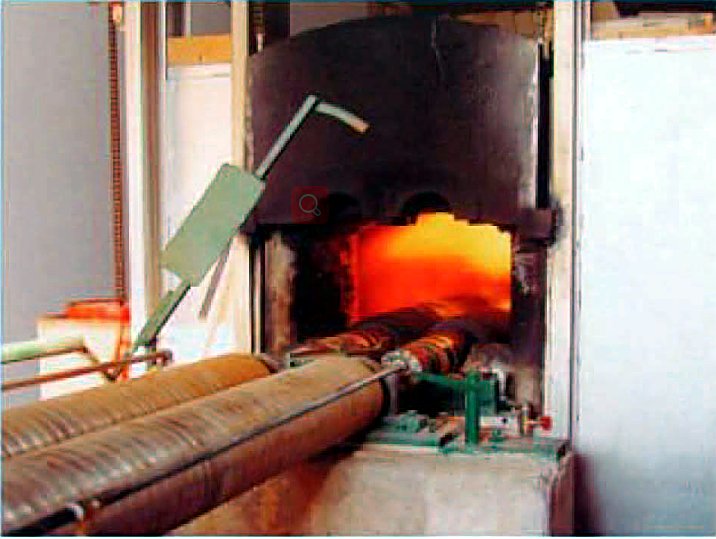
| Lining Options | Bimetallic (2–5 mm) or gas-nitrided |
| Joint Design | Flanged, dowel-located joints for accurate alignment |
| Hardness | Bimetallic HRC 55–72 / nitrided HV 900–1020 |
| Supply Basis | Built to extruder model, drawing or worn sample |
Material and treatment are selected by the resin you process, filler content and expected service life.
The kneading zone wears fastest — bimetallic lining extends the interval between replacements.
Cost-effective choice for low-abrasion positions along the barrel.
Different lining per position: bimetallic only where wear concentrates.
Dowel-located flanges keep bores aligned across the whole barrel length.
Correct bolts, nuts and clamps supplied together with segment sets.
Each segment inspected individually, then fit-checked as a complete assembly.
Common problems we help injection and extrusion plants solve — and how a matched screw barrel fixes them.
One worn zone forces replacement of the entire barrel on one-piece designs.
Segment design lets you replace only the worn section.Long lead times on complete barrels stop the line for weeks.
Spare segments on your shelf cut changeover to hours.Poorly machined joints misalign bores and scrub the screw.
Dowel-located, individually inspected segments keep alignment true.Kneading sections wear several times faster than feed sections.
Bimetallic-lined kneading segments built for exactly that duty.Badly seated vent segments leak vacuum and clog with compound.
Machined vent seats and correct port geometry keep degassing stable.Segments mixed from different suppliers no longer fit each other.
We document your layout and keep the specification for repeat orders.You send the extruder model or your current segment layout.
We evaluate which sections need replacement and which are reusable.
Bimetallic or nitrided selected per position, not one-size-fits-all.
Segments machined individually with flange and dowel precision.
Segments assembled and bore alignment verified before packing.
Marked per position, rust-protected, packed in wooden cases.
Segment barrels for pigment and additive masterbatch lines.
Glass-fibre and mineral-filled PA, PP and PBT compounding.
Twin screw segments for powder coating extruders.
Sections for regrind and washed-flake compounding lines.
Segmented barrels for adhesive and sealant extrusion.
Segments for heavily filled masterbatch formulations.
Small-diameter segment sets for laboratory compounding.
Segment packages supplied to twin screw extruder manufacturers.
Scheduled segment replacement to keep compounding lines running.
“We now keep spare kneading segments on site. A changeover that used to take three weeks takes two days.”
Maintenance LeadMasterbatch producer“The segment numbering and packing list made reassembly straightforward. Fit was perfect.”
Workshop ManagerCompounding plant“They replaced only the two worn sections instead of selling us a full barrel. Honest and efficient.”
Purchasing ManagerRecycling companyYes. We build to the extruder model, your drawing, or a worn sample. Common international brands and Chinese-built twin screw extruders are all workable.
Usually only the high-wear kneading and metering zones justify bimetallic lining; feed and conveying sections can be nitrided. We plan the layout with you based on your formula.
If your existing sections are still within tolerance, yes — we machine new segments to match your joint dimensions. Send measurements or a worn section for confirmation.
We document your segment layout after the first order, so repeat segments are a quick reorder with guaranteed fit.
Bore diameter, flange flatness and dowel positions are machined so the assembled barrel meets the same straightness tolerance as a one-piece barrel — typically within 0.05 mm over the full length.
Typically 25–40 days depending on quantity and lining. Individual replacement segments are often faster.
Send the drawing, machine model or worn sample — we confirm the geometry and quote within one working day.
Tell us the machine model, screw diameter and material you process — we will reply with a matched solution and quotation.
Or write directly to info@xiwangindustry.com · WhatsApp +86-13503734287
Segmented construction lets you replace the worn flight section instead of the whole screw, and lets you change the mixing configuration for a different product. If you run varied formulations or keep spares inventory low, modular usually pays for itself.
Yes. Individual flight elements, kneading blocks and barrel segments are supplied to your existing shaft and housing dimensions, so an order can be one element or a complete rebuild.
Segments are machined with controlled face squareness and assembled on a mandrel to check cumulative runout before shipment. A stack of individually accurate parts can still add up to a crooked assembly, so the assembled stack is what we measure.
Tell us your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.