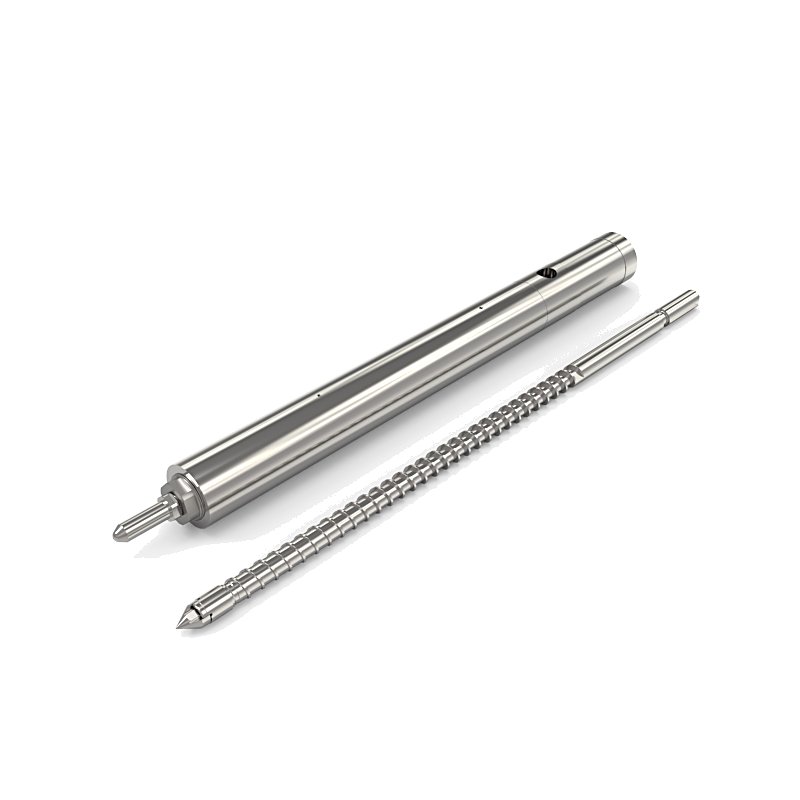
Why We Keep Nitriding and Alloy Casting Inside Our Own Workshop

Heat treatment decides how long a screw barrel lasts. Keeping it in-house decides how consistent that life is from order to order.

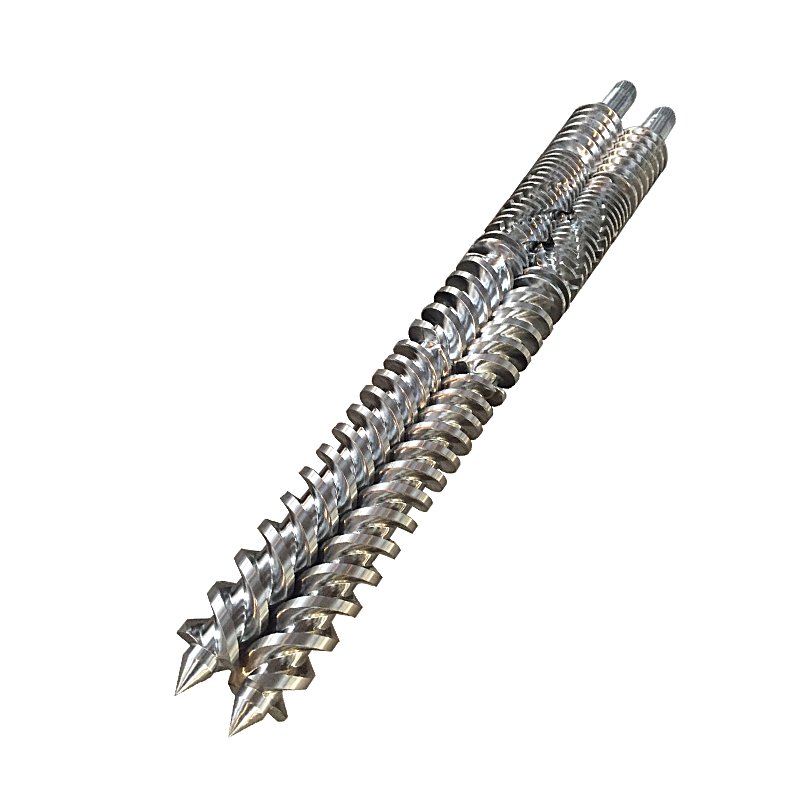
Anyone can buy machining hours. Heat treatment is different: the furnace cycle decides case depth, hardness profile and ultimately the service life of your screw and barrel. We run both processes in our own 14,000 m2 plant in Jiaozuo, Henan.
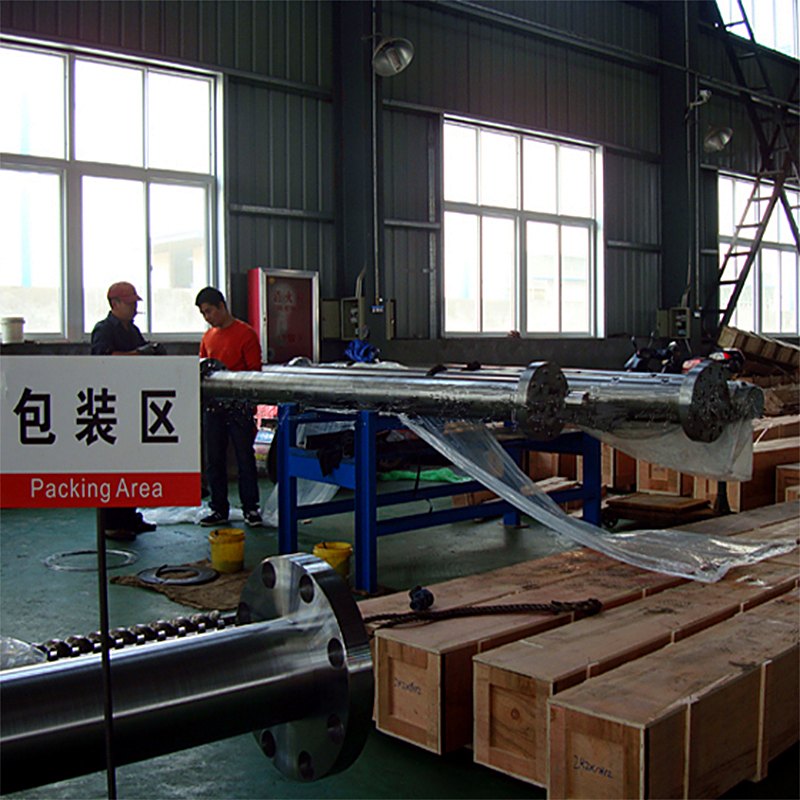
Heat treatment furnace in the Xiwang workshop

What we actually run

  • 4 gas nitriding furnaces for 38CrMoAlA screws and barrels
  • 4 fully automatic centrifugal bimetallic casting furnaces with Japanese Fuji high-temperature computer controllers
  • German super-hard deep-hole reaming for barrel bores, thread milling, grinding and polishing
  • Leeb hardness testers and alloy-layer thickness testing for verification

Why subcontracting heat treatment is a problem

A subcontractor gives you a certificate, not control. When a batch comes back at the low end of the hardness range you find out after machining is finished and the delivery promise is already made. Running the furnaces ourselves means the hardness and case depth are checked while the part is still ours to fix.

What it means for you

  • Traceability: every part leaves with its heat number and hardness readings
  • Consistency: the same cycle, the same result, the next time you reorder
  • Lead time: no queue behind someone else's order
  • Honest advice: because we pay for the cycle ourselves, we will tell you when you do not need the expensive option
Maximum machining diameter is Ø300 mm. Above that we tell you upfront that we cannot do it rather than quoting something we cannot hold tolerance on.
Send Inquiry → WhatsApp +86-13503734287

Related pages

Bimetallic Screw Barrels Factory Tour About Us
Keep Reading

More News and Technical Notes

Talk to the Team That Wrote This

Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.