Film-grade screw barrel for LDPE / LLDPE / HDPE blown film with stable, cool melt. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
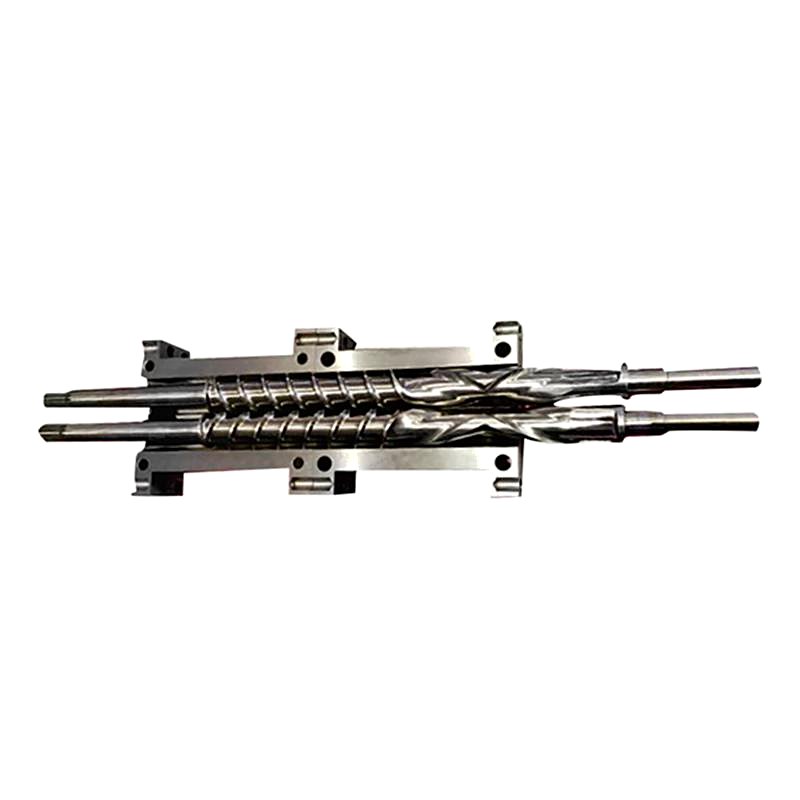
Film gauge variation is mostly a melt-stability problem. Our blown film screws use a dedicated film profile — deep feed, gentle compression and a distributive mixing section — so the melt arrives at the die at a flat, cool temperature and the frost line stays put.
Supplied for mono-layer and multi-layer lines processing LDPE, LLDPE, HDPE and EVA, from mini film extruders to Ø120 heavy-duty lines. Tell us your resin blend and die size and we match the geometry.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø35–120 mm |
|---|---|
| L/D ratio | 28–32 |
| Design | Film profile + distributive mixing tip |
| Melt temperature | Low and flat for gauge stability |
| Material | 38CrMoAlA nitrided; bimetallic for recycled blend |
| Output stability | ±2–3% at working point |
| Lead time | 30–40 days |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
Often, yes: a worn flight land or a badly designed mixing section pulses the melt. We can usually diagnose from your extruder model, resin and output readings — send them and we will tell you honestly whether the screw is the culprit.
Within limits. A film screw tuned for LLDPE (higher shear tolerance) runs LDPE acceptably; tell us your main blend and we optimise for it.
Yes, for HDPE film on high-output lines; for LDPE/LLDPE smooth bore remains the standard.
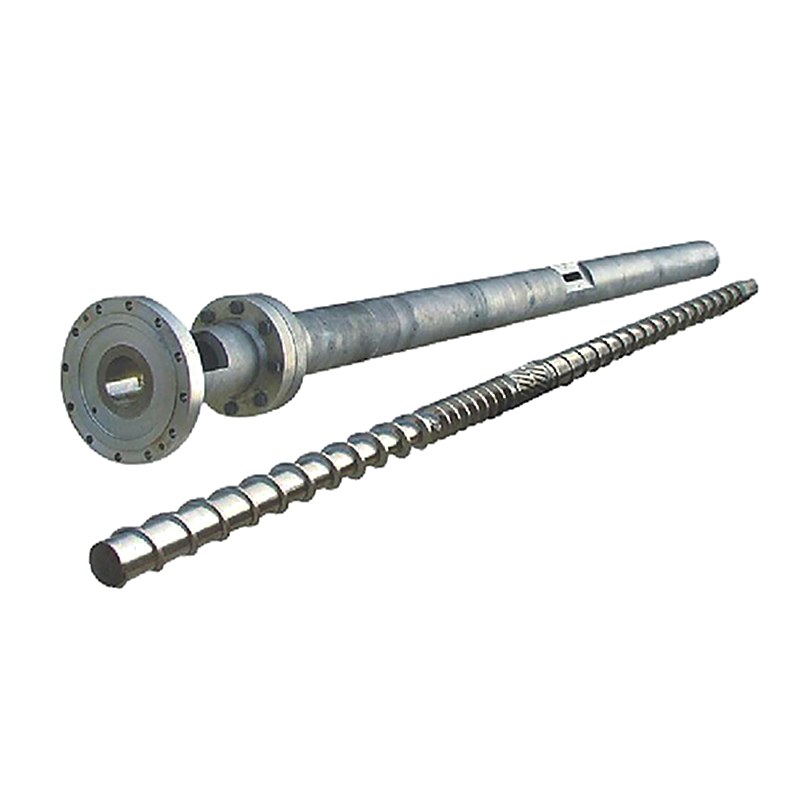
Complete set for PE/PP pipe, film, sheet and pelletizing extrusion lines.
View Details →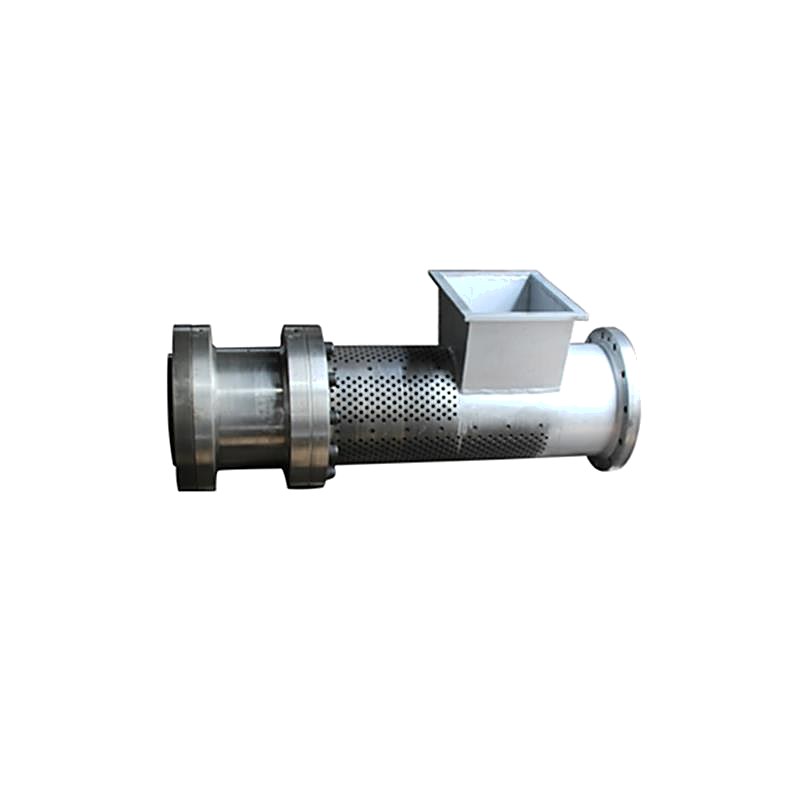
Degassing barrel with vent port for LDPE/HDPE with moisture or volatile content.
View Details →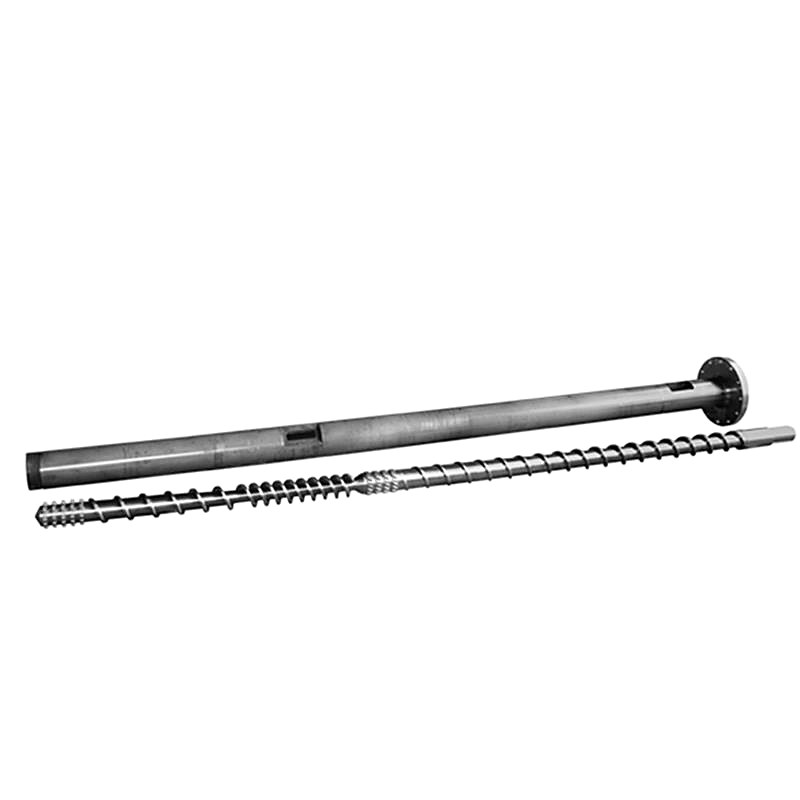
Grooved feed section for high-output HDPE pipe extrusion.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.