Mixing-head screw for blown film and cast film lines. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
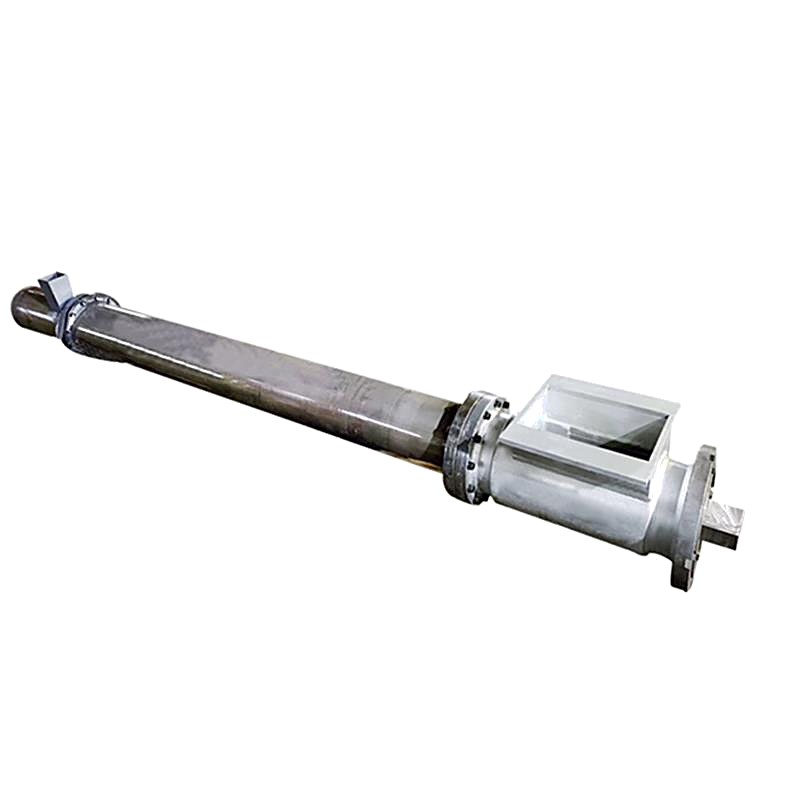
Film lives or dies on melt homogeneity. A mixing head breaks up unmolten gel particles and evens out temperature before the melt reaches the die, which is what stops gels and gauge bands showing up in the finished roll.
We specify the mixing section for your polymer — a gentle dispersive design for LDPE, something more distributive for LLDPE blends and metallocene grades.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø35–150 mm |
|---|---|
| L/D ratio | 24–32 |
| Mixing section | Distributive / dispersive, matched to resin |
| Material | 38CrMoAlA nitrided |
| Finish | Polished channels, chrome optional |
| Typical resins | LDPE, LLDPE, HDPE, PP, mPE |
| Lead time | 25–35 days |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
A correct mixing section removes most unmolten material. Persistent gels usually point to die build-up or a temperature profile issue, and we will say so rather than sell you a screw.
Yes — send the resin, output and current screw drawing and we match or improve it.
Nitrided for virgin PE/PP. Bimetallic only if you run heavy CaCO3 or recycle content.
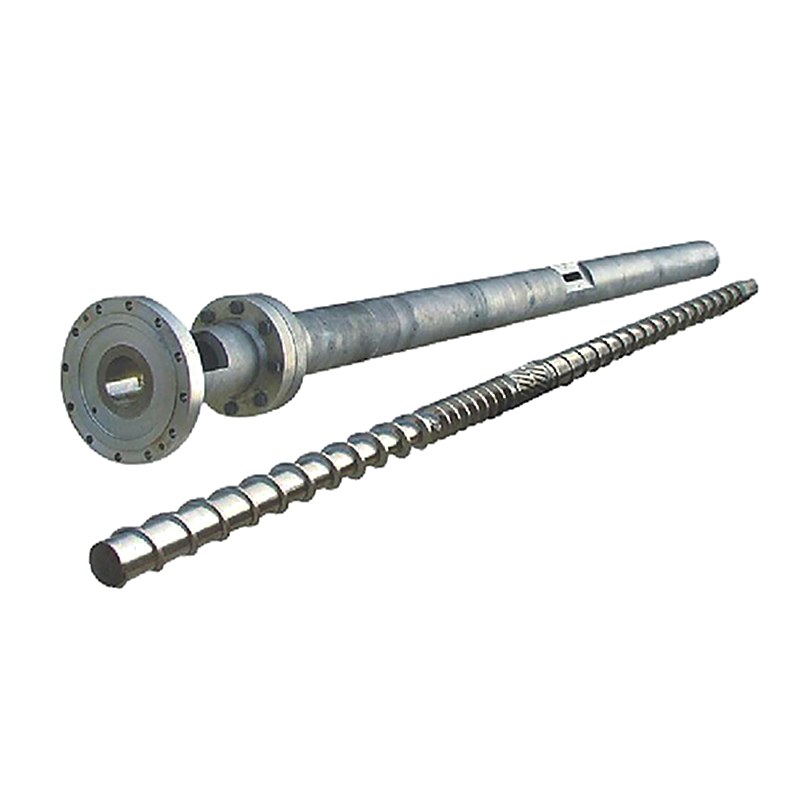
Complete set for PE/PP pipe, film, sheet and pelletizing extrusion lines.
View Details →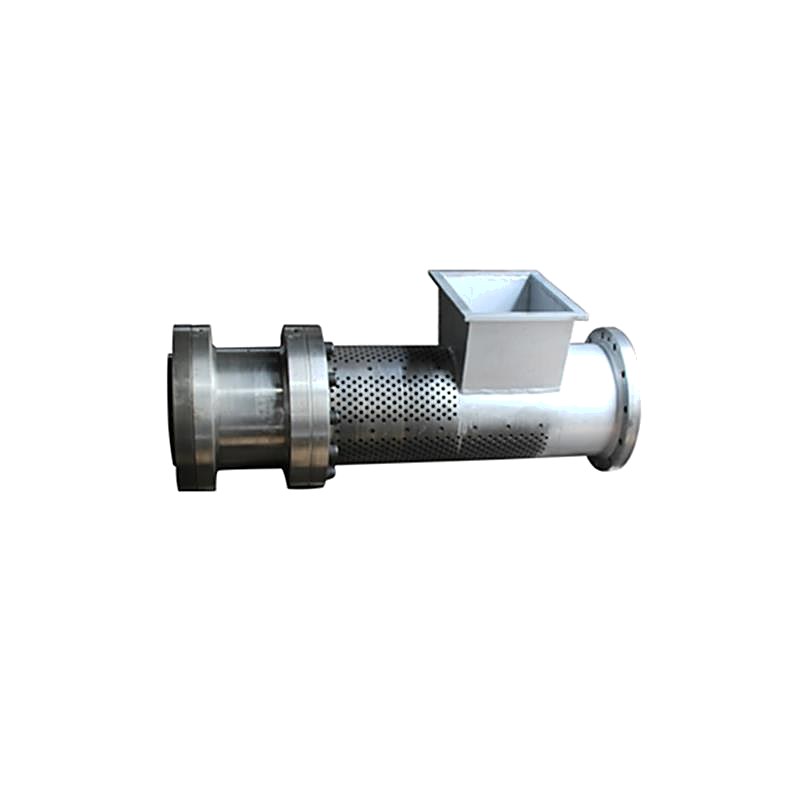
Degassing barrel with vent port for LDPE/HDPE with moisture or volatile content.
View Details →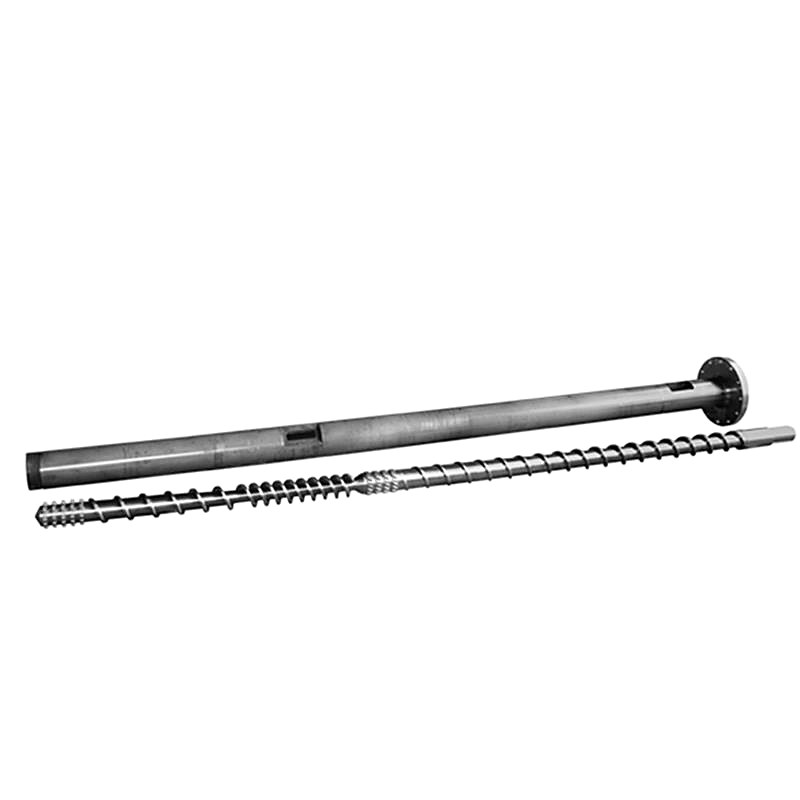
Grooved feed section for high-output HDPE pipe extrusion.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.