Bimetallic screw barrel for LDPE / PP / PET recycling and pelletising lines. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
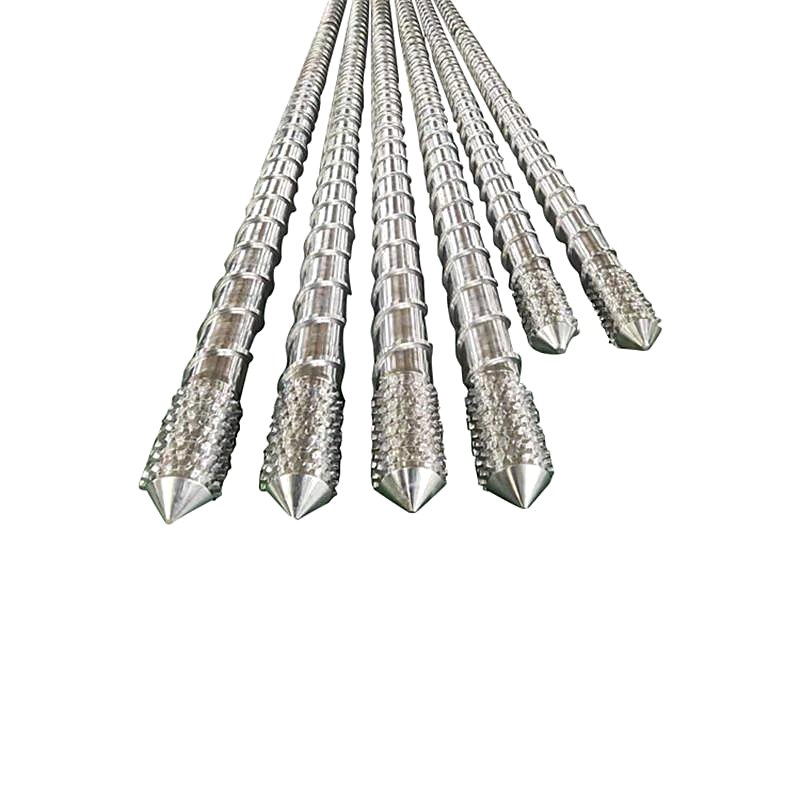
Recycled feed is sand, paper, aluminium and unknown fillers suspended in plastic — the fastest way to destroy a standard screw. Our recycling package pairs a bimetallic barrel (2–5 mm alloy lining) with a wear-protected screw and a vented two-stage option for wet or printed feed.
Built for LDPE film washing lines, PP woven-bag granulation and PET flake pelletising. Tell us your feed (washed film, flakes, rigid scrap) and moisture level and we configure the vent and screw compression.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø90–250 mm |
|---|---|
| L/D ratio | 28–36 (vented two-stage available) |
| Barrel | Bimetallic lining 2–5 mm, centrifugally cast |
| Screw protection | Hardened lands, Stellite option |
| Vent | Double-dump or single vent, vacuum-assisted |
| Expected life | 3–5× nitrided on contaminated feed |
| Lead time | 35–45 days |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
If the feed is washed film, nitrided can survive; if it is post-consumer or unwashed, no — hard contaminants will cut a nitrided bore in months. The bimetallic lining pays for itself on the first barrel you do not have to replace.
Vented (two-stage) if your feed carries moisture or inks — it degasses before pelletising and prevents porous pellets. Dry, single-source regrind can run non-vented for higher output.
Yes — send the extruder brand, screw dimensions and an honest description of the feed. We quote a matching set including the vent configuration.
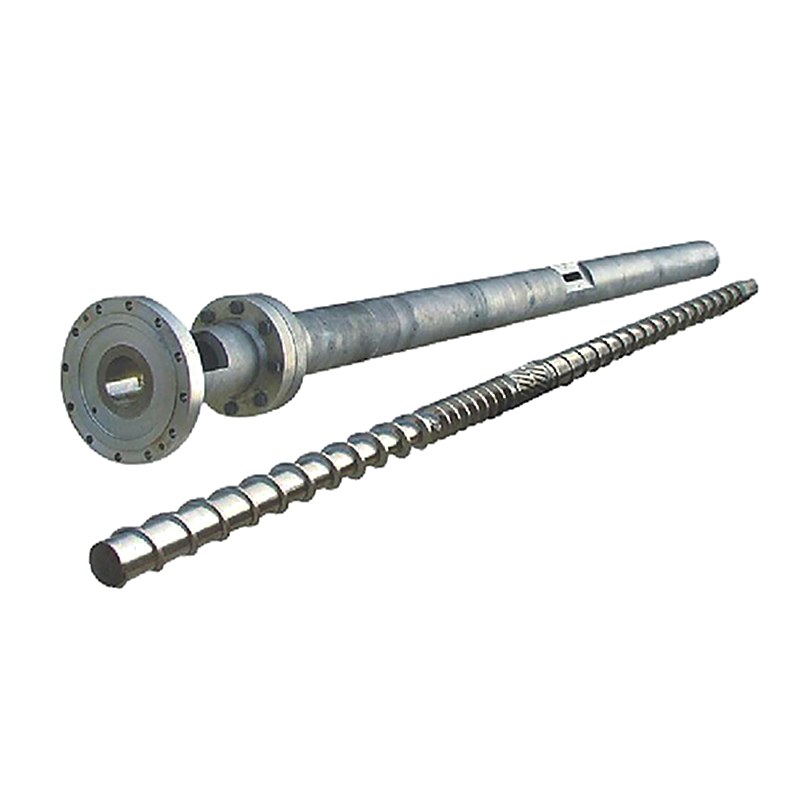
Complete set for PE/PP pipe, film, sheet and pelletizing extrusion lines.
View Details →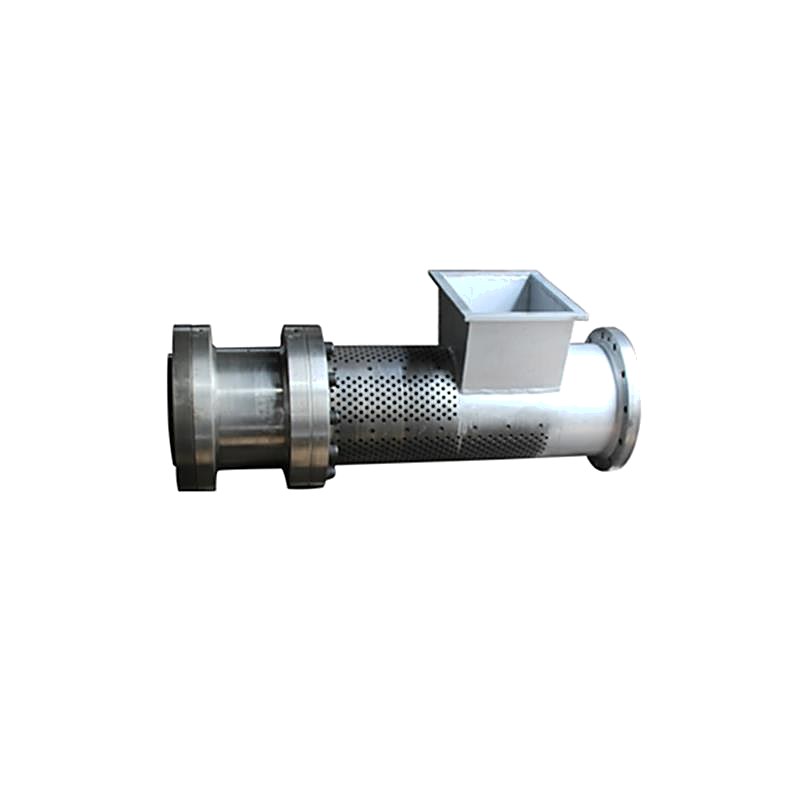
Degassing barrel with vent port for LDPE/HDPE with moisture or volatile content.
View Details →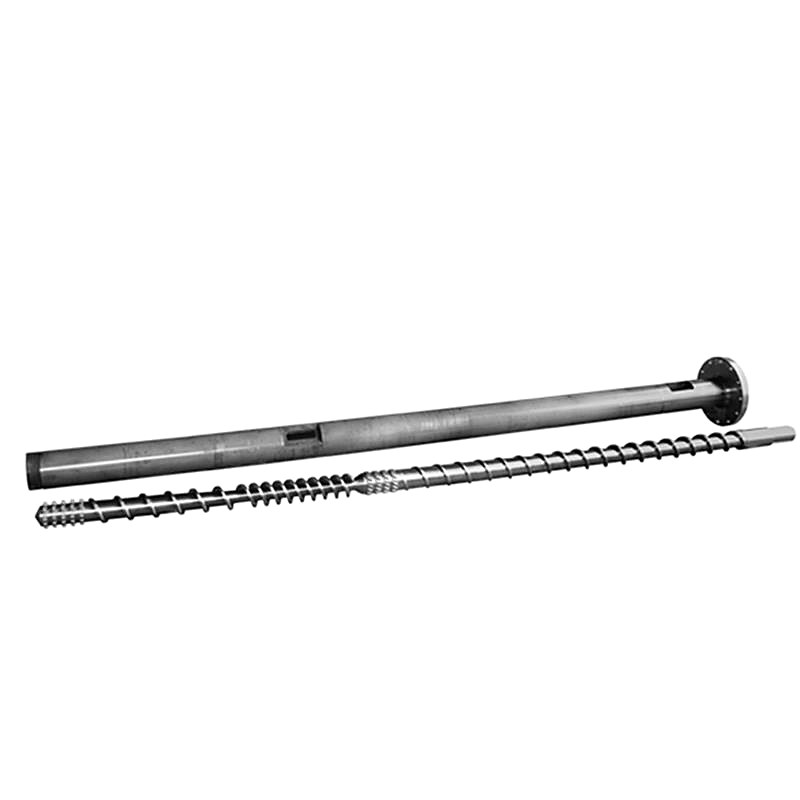
Grooved feed section for high-output HDPE pipe extrusion.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.