High-throughput screw barrel for thin-wall food packaging and fast-cycle moulding. Machined in our own Henan workshop — to your drawing, or reverse-engineered from your worn parts.
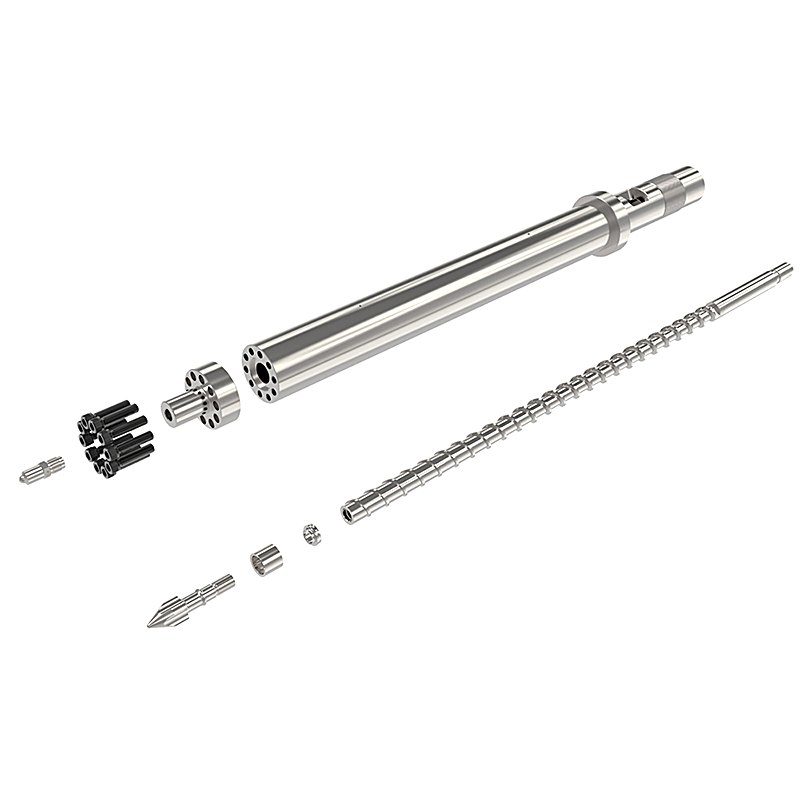
Thin-wall packaging is a plasticising race: the machine must melt a full shot in seconds and inject it before the tool freezes. Our thin-wall screw has a deep feed section and an aggressive melting section sized for fast cycle PP and PE, with check-ring non-return valves that keep shot weight consistent.
Built for deli containers, lids, cups and IML parts on high-speed machines. Send us the cycle time and shot weight and we will size the screw for the plasticising rate you actually need — not just the tonnage.
Quote within one business day. We reply with a matching proposal, delivery date and price — no generic catalogue PDF.
Standard range shown. Every dimension below can be changed to your machine, resin and output — custom manufacturing is our daily business.
| Screw diameter | Ø40–150 mm |
|---|---|
| Design | High-speed plasticising, quick-recovery profile |
| Non-return | Check-ring or ball valve, hardened |
| Material | 38CrMoAlA nitrided / bimetallic option |
| Hardness | HV 900–1020, depth 0.45–0.7 mm |
| Shot consistency | ±0.3–0.5% with matched valve |
| Lead time | 25–35 days |
The honest answer depends on your resin, not on price. Here is how we advise customers.
| Gas Nitrided (38CrMoAlA) | Bimetallic Alloy Lining | |
|---|---|---|
| Best for | Unfilled PE, PP, PS, ABS, virgin PVC | Glass-filled, mineral-filled, recycled, corrosive |
| Surface hardness | HV 900–1020, depth 0.45–0.7 mm | Alloy layer 2–5 mm, metallurgically bonded |
| Typical service life | Baseline | 3–5× baseline on abrasive resin |
| Cost | Lower | Higher, recovered through fewer stoppages |
| Certification | MTC with heat number | MTC + hardness records, third-party on request |
Recovery speed and melt homogeneity. The screw must deliver a fully molten, evenly coloured shot every 3–5 seconds; we deepen the feed and shorten the transition accordingly, and match the non-return valve so the shot does not drool or vary.
Yes, in most cases. Send the machine model and the current screw drawing or dimensions; we confirm the matching geometry before quoting.
Yes — valves, seats and tips are available individually or as matched sets with the screw.
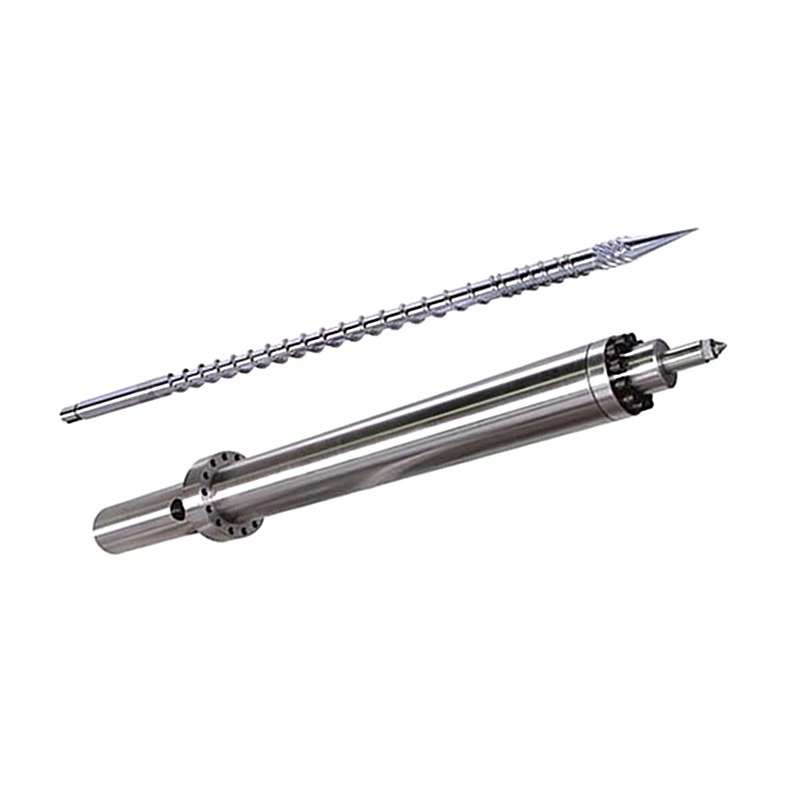
Complete matched set for 90–450 t injection moulding machines, nitrided or bimetallic.
View Details →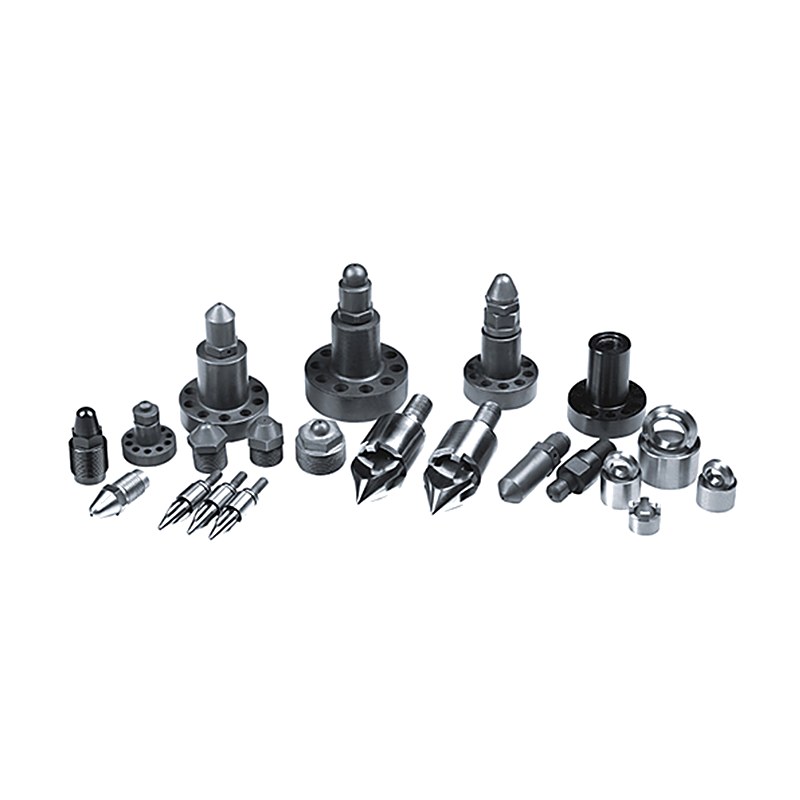
High-compression PET screw with barrier tips, low acetaldehyde generation for bottle-grade preforms.
View Details →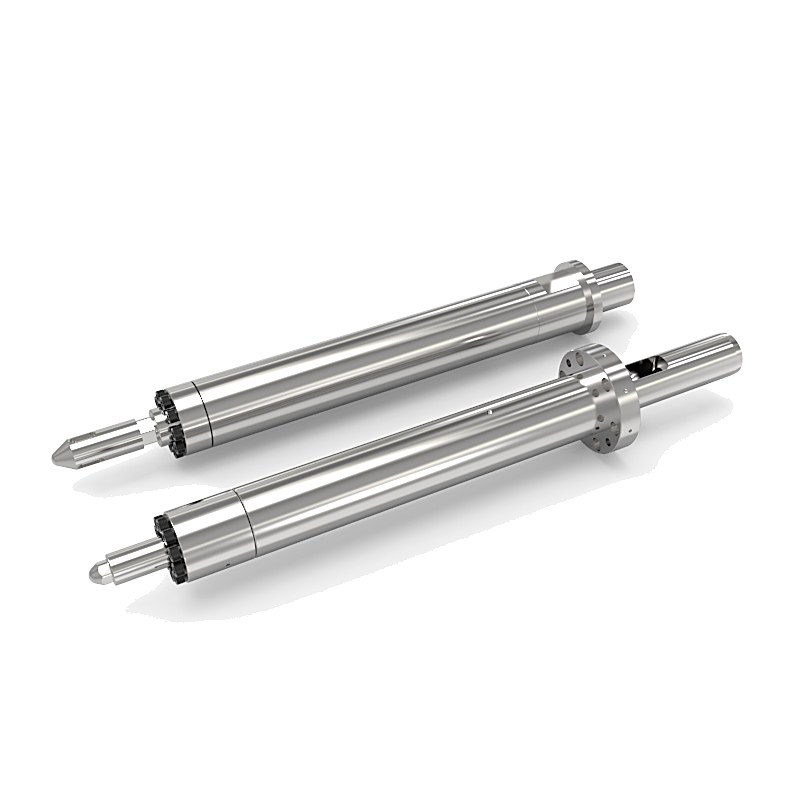
Centrifugally cast 2–5 mm alloy lining for glass-filled and corrosive resins.
View Details →Send your machine model, drawing or worn sample — we reply with a matching proposal and quotation within one business day.